-
-
-
-
SERVICE
-
JOIN US
-
CONTACT US


Operation Process for Machining Outer Circle and Inner Hole of Small CNC Lathe Parts
Release time:
2025-01-06
By implementing a reasonable clamping scheme, precise selection of positioning points, a scientific process route, appropriate tool selection, and effective CNC lathe programming and instructions, the external and internal hole machining of small CNC lathe parts can be carried out effectively. These steps and considerations together form the key elements to ensure processing quality and efficiency.
When processing parts on a small CNC lathe, a series of rigorous operational steps must be followed for the machining of the outer circle and inner hole. The following is a detailed operational process aimed at ensuring processing quality and efficiency.
1. Clamping Plan
First, choose a three-jaw self-centering chuck for clamping, with the positioning reference being the outer cylindrical surface of the blank. Since the part requires two clamping operations, a detailed clamping plan must be developed. During the first clamping, the outer cylindrical surface of the blank serves as the positioning reference, clamping the right end to process the left end; during the second clamping, the precision-turned outer circle serves as the positioning reference, using a soft jaw chuck for clamping to complete the shaping of the right end.
2. Position Point Selection
In the machining process, the selection of position points is crucial. For the processing of the left end, the intersection of the left end face and the axis is used as the workpiece coordinate origin; for the processing of the right end, the workpiece zero point is set on the right end face. Additionally, a tool change point and an inner hole turning cycle starting point must be set. In this example, the tool change point is set at (X100, Z100) as the starting point for the cycle; the inner hole turning cycle starting point is set at (X28, Z2).
3. Process Route
According to the principle of concentrating processes, the machining performed in one clamping is considered one process. Since this part requires two clamping operations to complete all machining, it is divided into two processes. The first process mainly processes the left end content, providing an accurate reference for the second process; the second process focuses on the machining of the right end content.
4. Tool Selection
The selection of tools directly affects processing quality and efficiency. For the machining needs of this part, tools such as external circle cutters, groove cutters, inner hole turning tools, and twist drills need to be selected. Specifically, a 90° external circle turning tool can be used for outer circle machining, a 75° inner hole turning tool for inner hole machining, and a groove cutter for groove machining. At the same time, the cutting parameters should also be adjusted based on factors such as processing materials, tool performance, and machine tool performance.
5. CNC Lathe Programming and Instructions
In CNC lathe programming, the reasonable use of outer circle machining cycle instructions can greatly simplify the programming process and improve processing efficiency. The specific use of instructions should be adjusted according to the machining needs of the part and the performance of the machine tool. For example, when machining the outer circle, cycle instructions can be used to achieve automatic feeding and retracting, thus saving time and improving machining accuracy.
By implementing a reasonable clamping plan, precise position point selection, a scientific process route, appropriate tool selection, and effective CNC lathe programming and instructions, the outer circle and inner hole machining of small CNC lathe parts can be effectively carried out. These steps and considerations together constitute the key elements to ensure processing quality and efficiency.
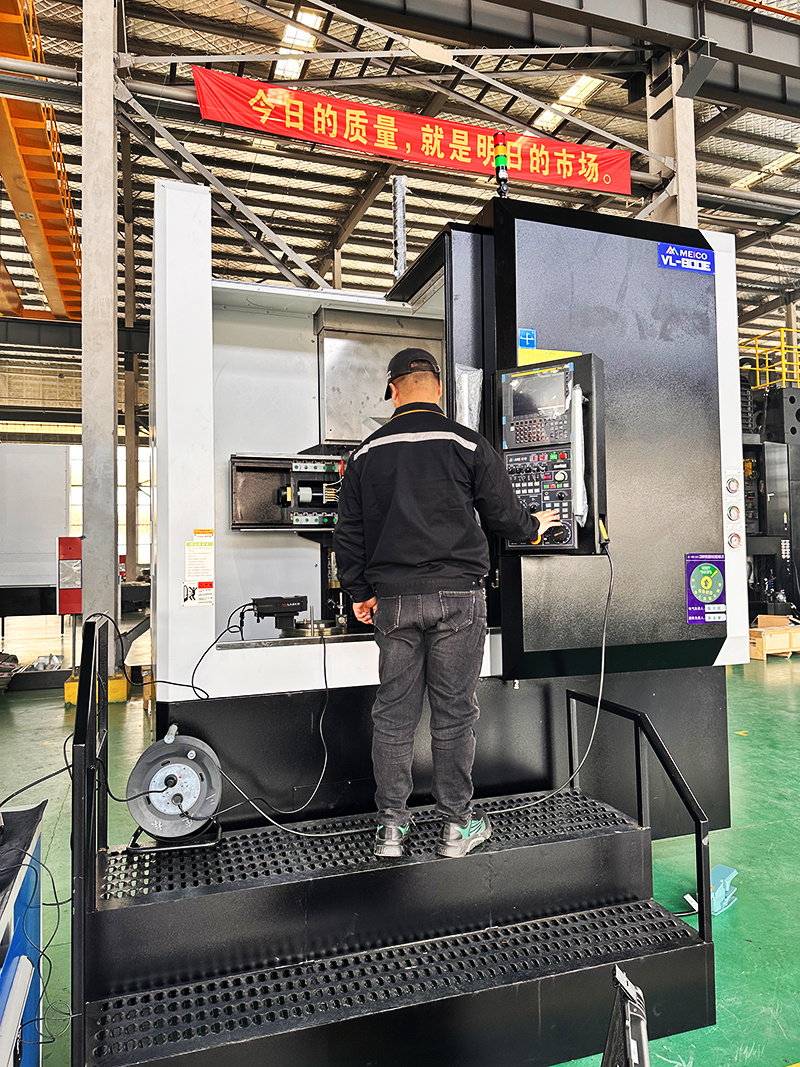
Meishenmeike small CNC vertical lathe, high precision, high rigidity, high stability, heavy cutting, to meet your production needs.



E-mail:meishenmeike@163.com
Zip Code: 226600
Add: No.68,Huangziliang Rd,Qutang Town, Hai'an City,Jiangsu
MEICO
Follow us